
Conveyor Roller

Conveyor Roller | N.M Enterprises Key Takeaways High-quality Conveyor Rollers improve efficiency and reduce downtime Choosing the right Conveyor Roller Manufacturer in India ensures long-term reliability Different industries require different types of conveyor rollers Working with an experienced Conveyor Roller Supplier improves operational performance Premium-quality rollers reduce maintenance and replacement costs over time In today’s fast-moving industrial environment, conveyor systems play a major role in improving productivity and streamlining material handling operations. At the heart of every efficient conveyor system is a critical component that often goes unnoticed — the Conveyor Roller. Although conveyor rollers may appear simple, they are responsible for ensuring smooth, safe, and uninterrupted movement of materials across industries. Selecting the right Conveyor Roller Manufacturer in India is not just about pricing; it is about reliability, durability, and long-term performance. At N.M Enterprises, we provide high-quality Conveyor Rollers designed for industrial performance, heavy-duty usage, and long operational life. Understanding the Importance of Conveyor Rollers What is a Conveyor Roller? A Conveyor Roller is a cylindrical mechanical component used in conveyor systems to transport products and materials from one location to another efficiently. These rollers are widely used in industries such as manufacturing, warehousing, logistics, packaging, mining, food processing, and material handling. Conveyor rollers continuously operate under demanding conditions including: Heavy load handling High-speed movement Dust and moisture exposure Continuous friction Industrial wear and tear A low-quality roller can result in conveyor failure, production delays, increased maintenance, and costly downtime. That is why selecting an experienced Conveyor Roller Supplier in India is essential for smooth operations. Why Quality Conveyor Rollers Matter Many businesses underestimate the importance of conveyor rollers and consider them standard replacement parts. However, poor-quality rollers can negatively affect the entire conveyor system. Problems Caused by Low-Quality Conveyor Rollers Frequent conveyor breakdowns Increased maintenance expenses Higher power consumption Reduced operational efficiency Excessive noise and vibration Shorter conveyor system lifespan At N.M Enterprises, we manufacture Conveyor Rollers using high-grade materials and precision engineering to deliver consistent performance and long-lasting durability. Key Features of High-Quality Conveyor Rollers Heavy-Duty Construction Our Conveyor Rollers are manufactured using premium-grade steel and industrial materials capable of handling demanding applications. Precision Engineering Accurate dimensions and proper balancing ensure smooth conveyor movement and improved efficiency. Smooth & Low Noise Operation Well-designed rollers reduce vibration and noise levels, improving workplace productivity and operator comfort. Corrosion Resistance Our rollers are designed to resist rust, moisture, chemicals, and harsh industrial conditions. High Load Capacity N.M Enterprises Conveyor Rollers are suitable for light-duty to heavy-duty material handling applications. Applications of Conveyor Rollers Our Conveyor Rollers are widely used across multiple industries: Manufacturing Industry Used in assembly lines, production systems, and packaging units for smooth product movement. Warehousing & Logistics Improves material handling efficiency in warehouses and distribution centers. Mining & Cement Industry Designed to withstand heavy loads and rough operating environments. Food Processing Industry Suitable for hygienic applications requiring smooth and corrosion-resistant rollers. Packaging Industry Ensures fast and efficient movement of cartons, boxes, and packaged goods. How to Choose the Right Conveyor Roller Manufacturer in India Choosing the right supplier directly affects operational efficiency and maintenance costs. Industry Experience An experienced Conveyor Roller Manufacturer understands industrial challenges and provides reliable solutions. Customization Capability Every conveyor system has unique requirements. We offer customized roller solutions based on application needs. Quality Assurance At N.M Enterprises, every Conveyor Roller undergoes strict quality inspection and performance testing. Technical Support We provide complete support including product guidance, technical assistance, and after-sales service. Transparent Communication We ensure timely delivery, professional service, and clear communication throughout the project. Why Conveyor Rollers Affect Your Business Performance Investing in premium Conveyor Rollers helps businesses achieve: Reduced operational downtime Lower maintenance costs Improved conveyor efficiency Smooth material handling Increased productivity Longer equipment life High-quality Conveyor Rollers are not just components — they are long-term investments for industrial growth and efficiency. Why Choose N.M Enterprises? N.M Enterprises is a trusted Conveyor Roller Manufacturer and Supplier in India, delivering reliable and cost-effective material handling solutions for various industries. Our Strengths High-quality industrial Conveyor Rollers Customized roller manufacturing solutions Competitive pricing Durable and precision-engineered products Fast delivery and professional support Strong focus on customer satisfaction We understand industrial requirements and provide Conveyor Rollers designed for long-lasting performance and maximum efficiency. Conclusion Selecting the right Conveyor Roller Manufacturer in India plays a crucial role in ensuring smooth industrial operations and long-term reliability. At N.M Enterprises, we are committed to delivering premium-quality Conveyor Rollers that improve productivity, reduce maintenance, and enhance operational efficiency. Whether you require rollers for warehousing, manufacturing, logistics, packaging, or heavy-duty industrial applications, we provide dependable solutions tailored to your requirements. Contact N.M Enterprises today for high-performance Conveyor Roller solutions designed for modern industries.
Flexible Gravity Conveyor
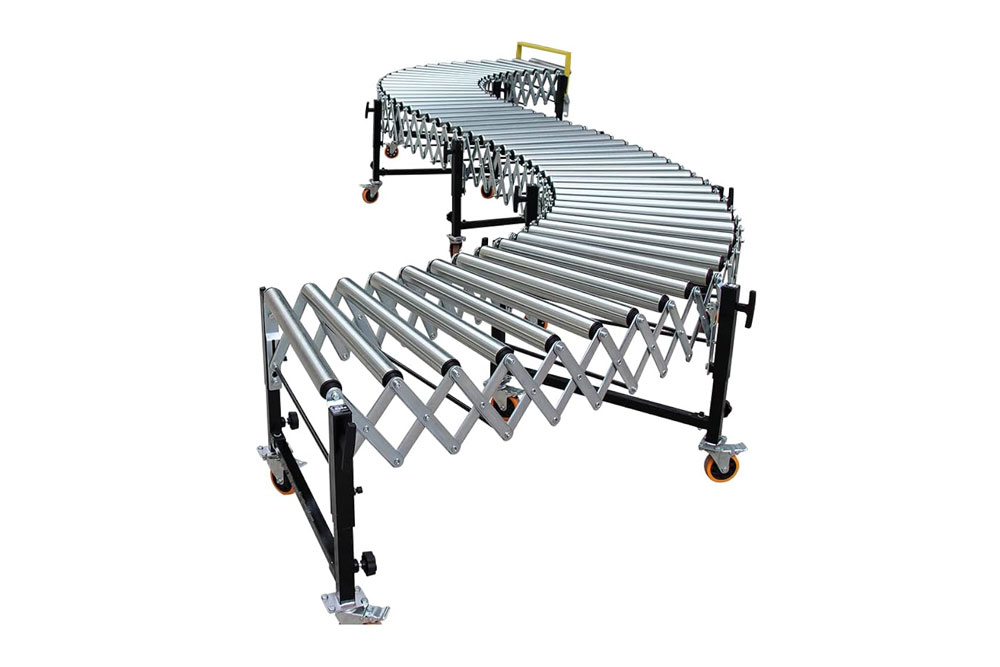
Gravity Conveyor: Introduction, Uses, Advantages, and Limitations A gravity conveyor is one of the most widely used material handling solutions in warehouses, manufacturing facilities, and distribution centers. A gravity conveyor system operates using gravity or manual force to move cartons, boxes, and packages from one point to another without requiring motors or electricity. Typically, the system consists of rollers or skate wheels mounted on a sturdy frame that allows products to move smoothly across the conveyor line. Due to its simple design and affordability, the gravity roller conveyor is commonly used in logistics, packaging, and assembly operations. Many businesses prefer gravity conveyors because they provide a cost-effective conveyor system that improves workflow efficiency while reducing operational costs. Uses of Gravity Conveyor The main gravity conveyor uses include short-distance transportation of goods in packing stations, sorting areas, loading docks, and assembly lines. A warehouse gravity conveyor is ideal for moving cartons and lightweight products between workstations. These conveyors are also widely used in gravity conveyor for warehouses where layouts frequently change, as they are easy to relocate and expand. Advantages of Gravity Conveyor One of the major advantages of gravity conveyor systems is their low cost since they do not require motors or electrical components. They also require minimal maintenance and consume no energy, making them environmentally friendly. Additionally, a material handling gravity conveyor is flexible and easy to install in various industrial setups. Limitations of Gravity Conveyor Despite their benefits, there are some gravity conveyor limitations. They provide limited control over product speed and are not suitable for long-distance transportation. An industrial gravity conveyor system may also require manual effort and can be difficult to integrate with advanced automation technologies.
Powered Roller Conveyor
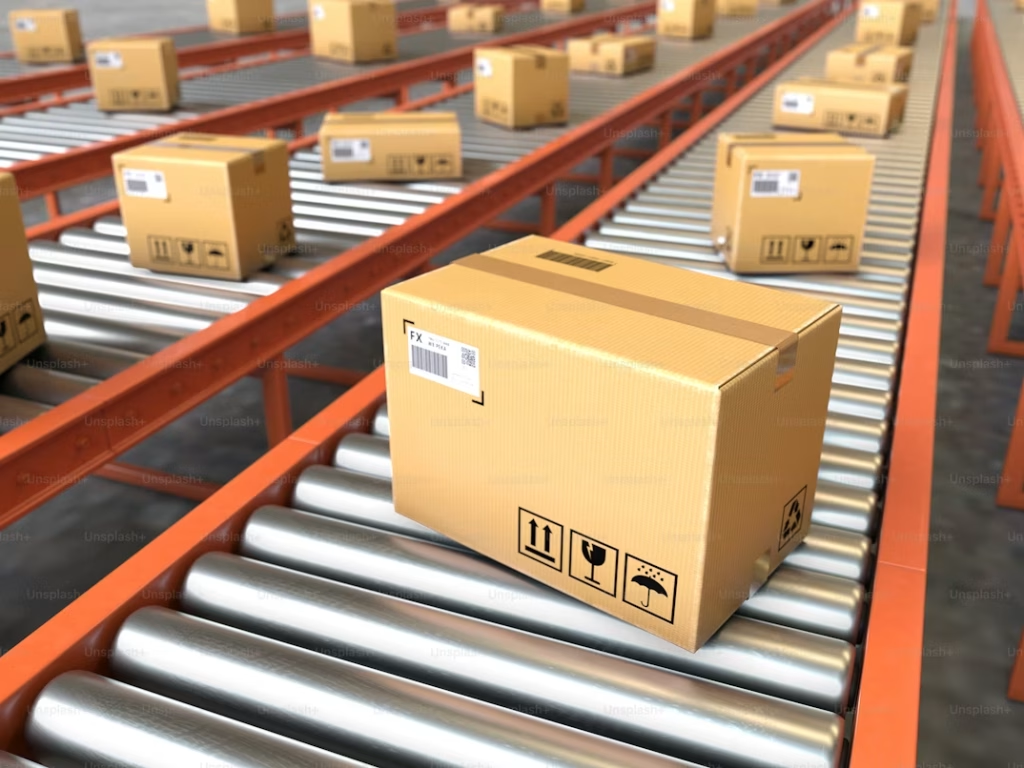
A powered roller conveyor is an advanced material handling system designed to transport goods efficiently using motor-driven rollers. Unlike gravity conveyors, this system uses electric motors, belts, or chains to rotate the rollers, enabling smooth and controlled movement of products across warehouses, manufacturing units, and distribution centers. It is widely recognized for its reliability, flexibility, and ability to handle various load types, including cartons, pallets, and totes. Advantages One of the key advantages of a powered roller conveyor is its ability to provide consistent and controlled product movement. With adjustable speed settings, it ensures safe handling and reduces the risk of product damage. Another major benefit is increased productivity, as powered roller conveyors allow continuous flow of materials, minimizing manual labor and operational delays. A powered roller conveyor also offers excellent scalability and flexibility. It can be easily customized with features like accumulation zones, sensors, and automated controls to suit specific operational needs. Additionally, these systems are energy-efficient and require relatively low maintenance, making them a cost-effective solution for long-term use. Integration is another strong advantage. A powered roller conveyor can seamlessly connect with warehouse automation systems such as barcode scanners, sorting systems, and robotic solutions, enhancing overall efficiency and accuracy. Uses Powered roller conveyors are extensively used in industries such as e-commerce, logistics, manufacturing, and packaging. They play a crucial role in sorting and distribution centers, where fast and accurate movement of goods is essential. In manufacturing plants, a powered roller conveyor is used to transport products between different stages of production. In warehouses, these conveyors help streamline order fulfillment processes by moving items quickly from storage areas to packing and shipping zones. Their ability to handle medium to heavy loads makes them ideal for pallet handling and bulk material transportation. Overall, It is a vital component in modern automated systems, offering efficiency, reliability, and improved operational performance.